What Is a Manufacturing Facility Electrical Upgrade?
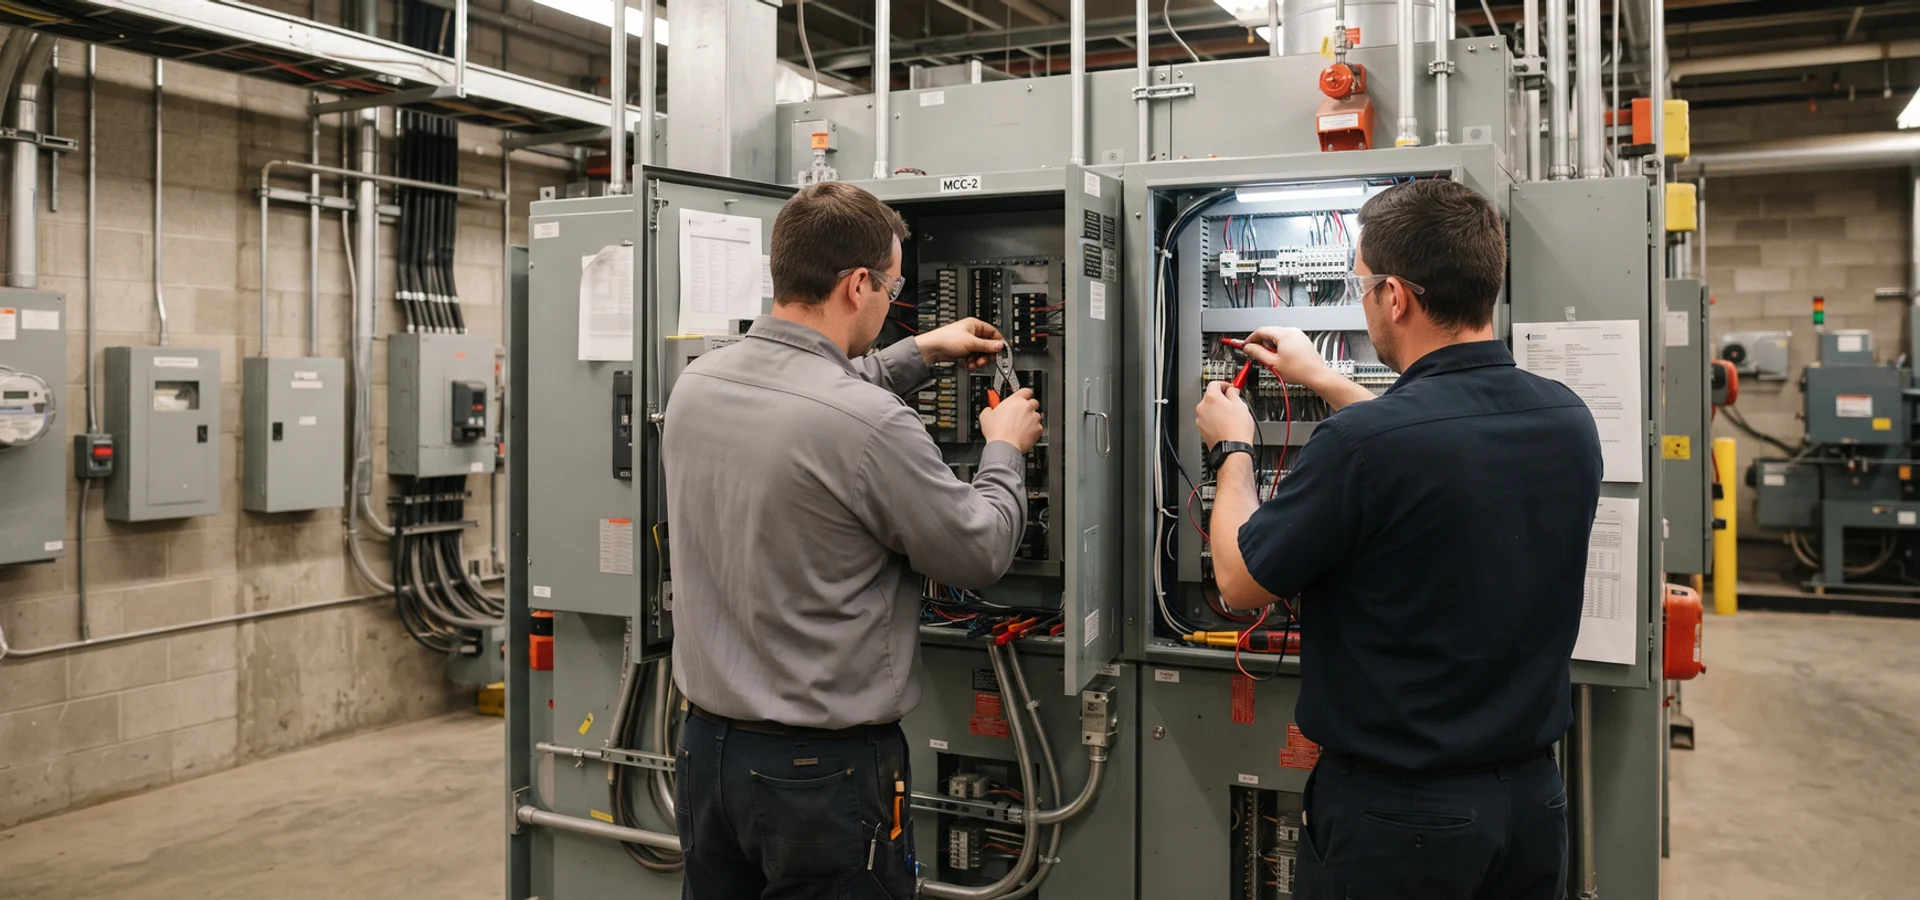
A manufacturing electrical upgrade adds and reorganises the distribution that feeds machine loads: switchgear sections, motor control centres, three-phase feeders to production cells, and local disconnects where maintenance needs to isolate equipment. The work is often driven by a cell expansion, a machine replacement whose nameplate exceeds the existing feeder, or a distribution system that has been extended repeatedly over the years until nothing has spare capacity.
What separates this from commercial distribution work is the load profile. Machine loads have high starting currents, varying duty cycles, and simultaneity patterns that depend on how the plant is actually run. Sizing on a nameplate sum over-specifies the equipment and the budget. Sizing without starting currents produces nuisance tripping the first time two machines start together. The load study has to model both, and the resulting design still has to satisfy the Ontario Electrical Safety Code (OESC) before ESA plan review clears it.
The second difference is the schedule. A production line has a value per hour, so the project is built around your shutdown calendar rather than the contractor’s convenience. Equipment gets set and feeders get pulled while the line runs. Transfers happen inside agreed windows.
For the industrial range, see industrial electrical panel upgrades.
Typical Scopes
- Machine feeders within existing distribution. New feeders and local disconnects for added or replaced equipment.
- Switchgear or MCC addition. New sections and buckets where the existing distribution has no spare capacity.
- Service and distribution upgrade. Where the load study exceeds the existing service. See three-phase electrical service upgrades.
- VFD feeder work. Correctly sized and routed feeds for variable frequency drives with proper bonding.
When a Plant Needs Distribution Work
- A machine replacement exceeds its existing feeder. New equipment nameplates are often higher than the equipment they replace.
- A cell is being added. New feeders, starters and disconnects, and a re-check of simultaneity across the plant.
- Breakers trip on simultaneous starts. The signature symptom of distribution sized on running current alone.
- The MCC has no spare buckets. The reason every subsequent equipment change becomes a project.
- Fault current has increased. After a service upgrade, equipment ratings need re-verification against the new available fault current.
- Maintenance cannot isolate equipment safely. Missing local disconnects is both an operational and a safety problem.
What Drives the Cost Between $5,000 and $15,000
Switchgear and MCC scope leads: new sections and buckets are the largest equipment items. Feeder count and routing is second, since every machine feeder is a conduit route with terminations and a disconnect. Shutdown constraints are third, because work compressed into short windows needs more crew for less time. SCCR remediation is fourth, where equipment ratings turn out to be inadequate for the available fault current and have to be addressed.
Utility infrastructure, where the service itself changes, is priced by the utility and quoted separately rather than absorbed into the contractor scope.
What to Expect Through the Project
The first phase is the load study and the paperwork: machine nameplate data, starting currents, duty cycles and simultaneity, growth allowance for planned equipment, then the single-line diagram, equipment ratings and available fault current verification for the commercial ESA plan review.
Installation is sequenced against your shutdown calendar. Switchgear and MCC sections are set and feeders pulled while the plant operates, because none of that work touches live circuits. Transfers, terminations into live distribution and the cutover happen inside the agreed windows.
Commissioning is done cell by cell. Phase rotation is verified and documented before the first start on every affected machine, loads are tested, and feeders are tagged. The ESA inspector attends, and maintenance receives tagged feeder records, MCC bucket schedules, the as-built single-line diagram, SCCR and rotation verification, the Certificate of Inspection and the itemised invoice.
Switchgear and Distribution for Manufacturing: Main Switchgear, MCC Sections, VFDs, and Process Feeders
A manufacturing facility carries load types that residential and commercial services do not have to consider. Main switchgear ratings, motor control centre sections, variable frequency drives, and process feeder isolation each get engineered independently for the plant’s actual production layout.
Main service switchgear
- Main switchgear sized to the plant total demand: typically 400-1600A three-phase 208V or three-phase 600V, from Eaton Pow-R-Line, Schneider Electric Square D I-Line or Siemens WL series.
- Short-circuit current rating (SCCR) verification: switchgear SCCR matched to the available fault current at the utility service, documented for ESA.
- Ground-fault protection on services 1000A and above: required by OESC Section 14.
- Metering and monitoring: utility metering plus internal power monitoring on Eaton IQ, Square D PowerLogic or Siemens SENTRON platforms.
Motor control centre (MCC) sections
- MCC line-up sized to the plant motor loads: Eaton Freedom 2100, Square D Model 6 or Siemens tiastar sections, typically 600A to 2500A bus rating.
- Combination starter buckets per motor: each MCC bucket holds a disconnect, motor starter, overload relay, and control transformer.
- Bucket labelling and machine tagging: each bucket labelled to the machine or cell it feeds, cross-referenced on the single-line and the MCC schedule.
- Spare bucket positions: typically 15-25% spare bucket positions for future machine additions.
Variable frequency drives (VFDs)
- VFD sizing to motor nameplate: Allen-Bradley PowerFlex, Yaskawa GA800, or ABB ACS580 drives sized 1:1 or one step above the motor.
- Line reactors and harmonic mitigation: required where multiple VFDs share a service, to keep harmonic distortion inside utility acceptance limits.
- VFD bypass circuits: allow the motor to run directly on line power if the drive fails, for continuous-process equipment.
- Motor cable and shielding: VFD-rated motor cable with shielding to control bearing currents and EMI on nearby control loops.
Process feeders and machine isolation
- Dedicated feeder per production cell or machine: sized to the machine’s connected load plus starting current, with local disconnect for maintenance.
- Local machine disconnect within sight of the equipment: OESC Section 28 requirement for maintenance isolation.
- Lockout-tagout provisions: each disconnect equipped for lockout with a locking hasp accessible from a standing position.
- Emergency stop circuit integration: wired to the plant safety controller with hard-wired backup, not through the machine PLC alone.